



Heat treatment temperature of DIN 17175 10CrMo910 Seamless Steel Tubes
| Steel Grade | Thermal processing ℃ | Normalizing℃ | Tempering | ||
| Grade | Material number | Quenching temperature ℃ | Tempering temperature ℃ | ||
| 10CrMo910 | 1.7380 | 1100 to 850°C | - | 900-960 | 700-750 |
Chemical composition of DIN 17175 10CrMo910
| Standard:DIN 17175 | grade | Chemical composition | |||||
| C | Si | Mn | P,S | Cr | Mo | ||
| 10CrMo910 | 0.08-0.15 | ≤0.50 | 0.40-0.70 | ≤0.030 | 2.00-2.50 | 0.90-1.20 | |
Mechanical property of DIN 17175 10CrMo910
| Standard | grade | Tensile Strength(MPa) | Yield Strength(MPa) | Elongation(%) |
| DIN 17175 | 10CrMo910 | 450-600 | ≥280 | ≥18 |
Dimensions Tolerance
| Project | Standard | Size range | Tolerance | |||
| Outer diameter | DIN17175 | Hot rolled steel pipe | OD ≤ 100mm | ± 0.75%( Min ± 0.5mm ) | ||
| OD> 100~ 320mm | ± 0.9% | |||||
| Cold drawn steel pipe OD ≤ 120mm | ± 0.6%( Min ± 0.25mm ) | |||||
| Wall thickness | DIN17175 | OD ≤ 130mm | WT ≤ 2Sn | +15%~-10% | ||
| WT > 2Sn~4Sn | +12.5%~-10% | |||||
| WT > 4Sn | ± 9% | |||||
| 130 < OD ≤ 320mm | WT ≤ 0.05OD | +17.5%~-12.5% | ||||
| 0.05OD < WT ≤ 0.11OD | ± 12.5% | |||||
| WT > 0.11OD | ± 10% | |||||
Original material test
A thin sheet should be taken at the top end of each round or square bar ingot for a pickling test to determine if the top end is adequately cut. Ultrasonic testing can also be performed on the shrinkage hole as selected by the supplier.
Test:
Chemical composition verification test
hydrostatictest
Tensile test
Notched impact test
Yield strength test
Ring test
Nondestructive testing
Tube flag
All steel pipes submitted for testing and acceptance shall be marked on the left and right sides of the pipe end at 300 mm. The mark is usually a number. Thin-walled tubes can also be used in other forms.
Welding properties of DIN 17175 10CrMo910 seamless alloy steel pipe
When DIN 17175 10CrMo910 alloy steel pipe is welded, if the welding rod and welding wire with the same strength as the base metal are selected, the plasticity of the welding joint obtained is poor, the preheating temperature is required to be 400-450 ℃, the preheating temperature is high, and the construction conditions are poor; in order to improve the plasticity of the welded joint, it is necessary to conduct 740 ℃ heat preservation for 3h high temperature tempering after welding. However, high temperature preheating and high temperature tempering for a long time will cause obvious softening of the HAZ.
If the electrode and welding wire with slightly lower strength and better plasticity are selected, the preheating temperature will be greatly reduced (actual operation 250-300 ℃), the high temperature tempering temperature will also be reduced, the tempering treatment time will be shortened, and 700-720 ℃ will be kept for 1H for tempering, which is enough to eliminate the welding stress and will not cause the softening of the heat affected zone of welding. Therefore, r317 electrode and h08crmoa welding wire are generally used for DIN 17175 10CrMo910 alloy steel pipe welding.
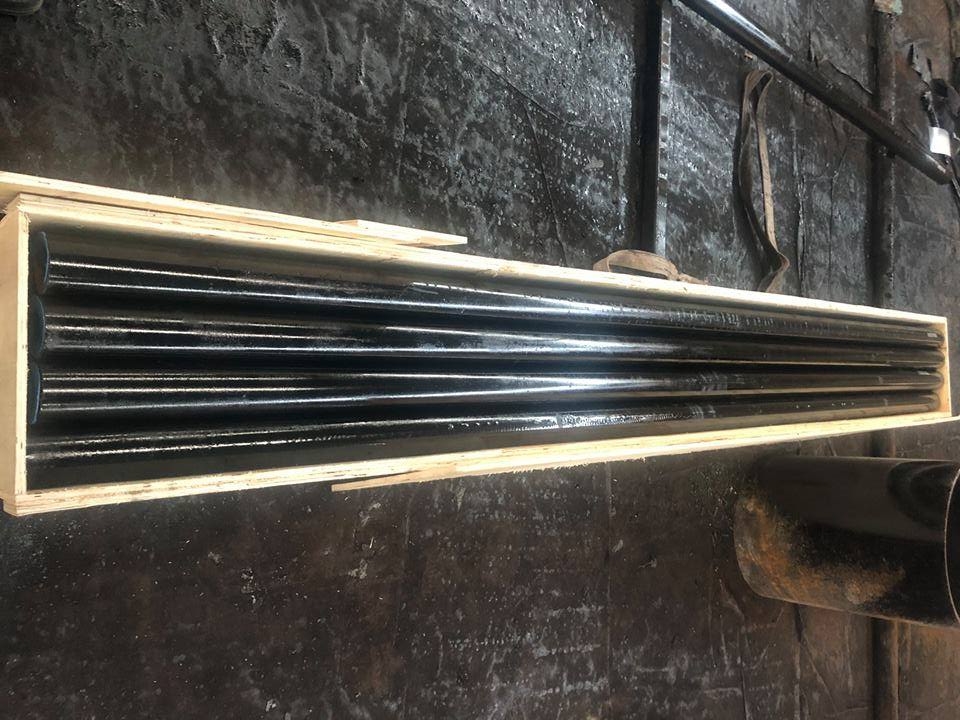
Photos of DIN 17175 10CrMo910 Seamless Steel Tubes

Hot Tags: heat treatment temperature of din 17175 10crmo910 seamless steel tubes, China heat treatment temperature of din 17175 10crmo910 seamless steel tubes manufacturers, suppliers, factory, Q195 Hot Dipped Galvanized Steel Tube, galvanized iron gi pipe, ASTM A53 Galvanized Steel Pipe, 4 Inch Galvanized Round Steel Pipe, galvanized pipe tube, Gi steel pipe


